

MBR System
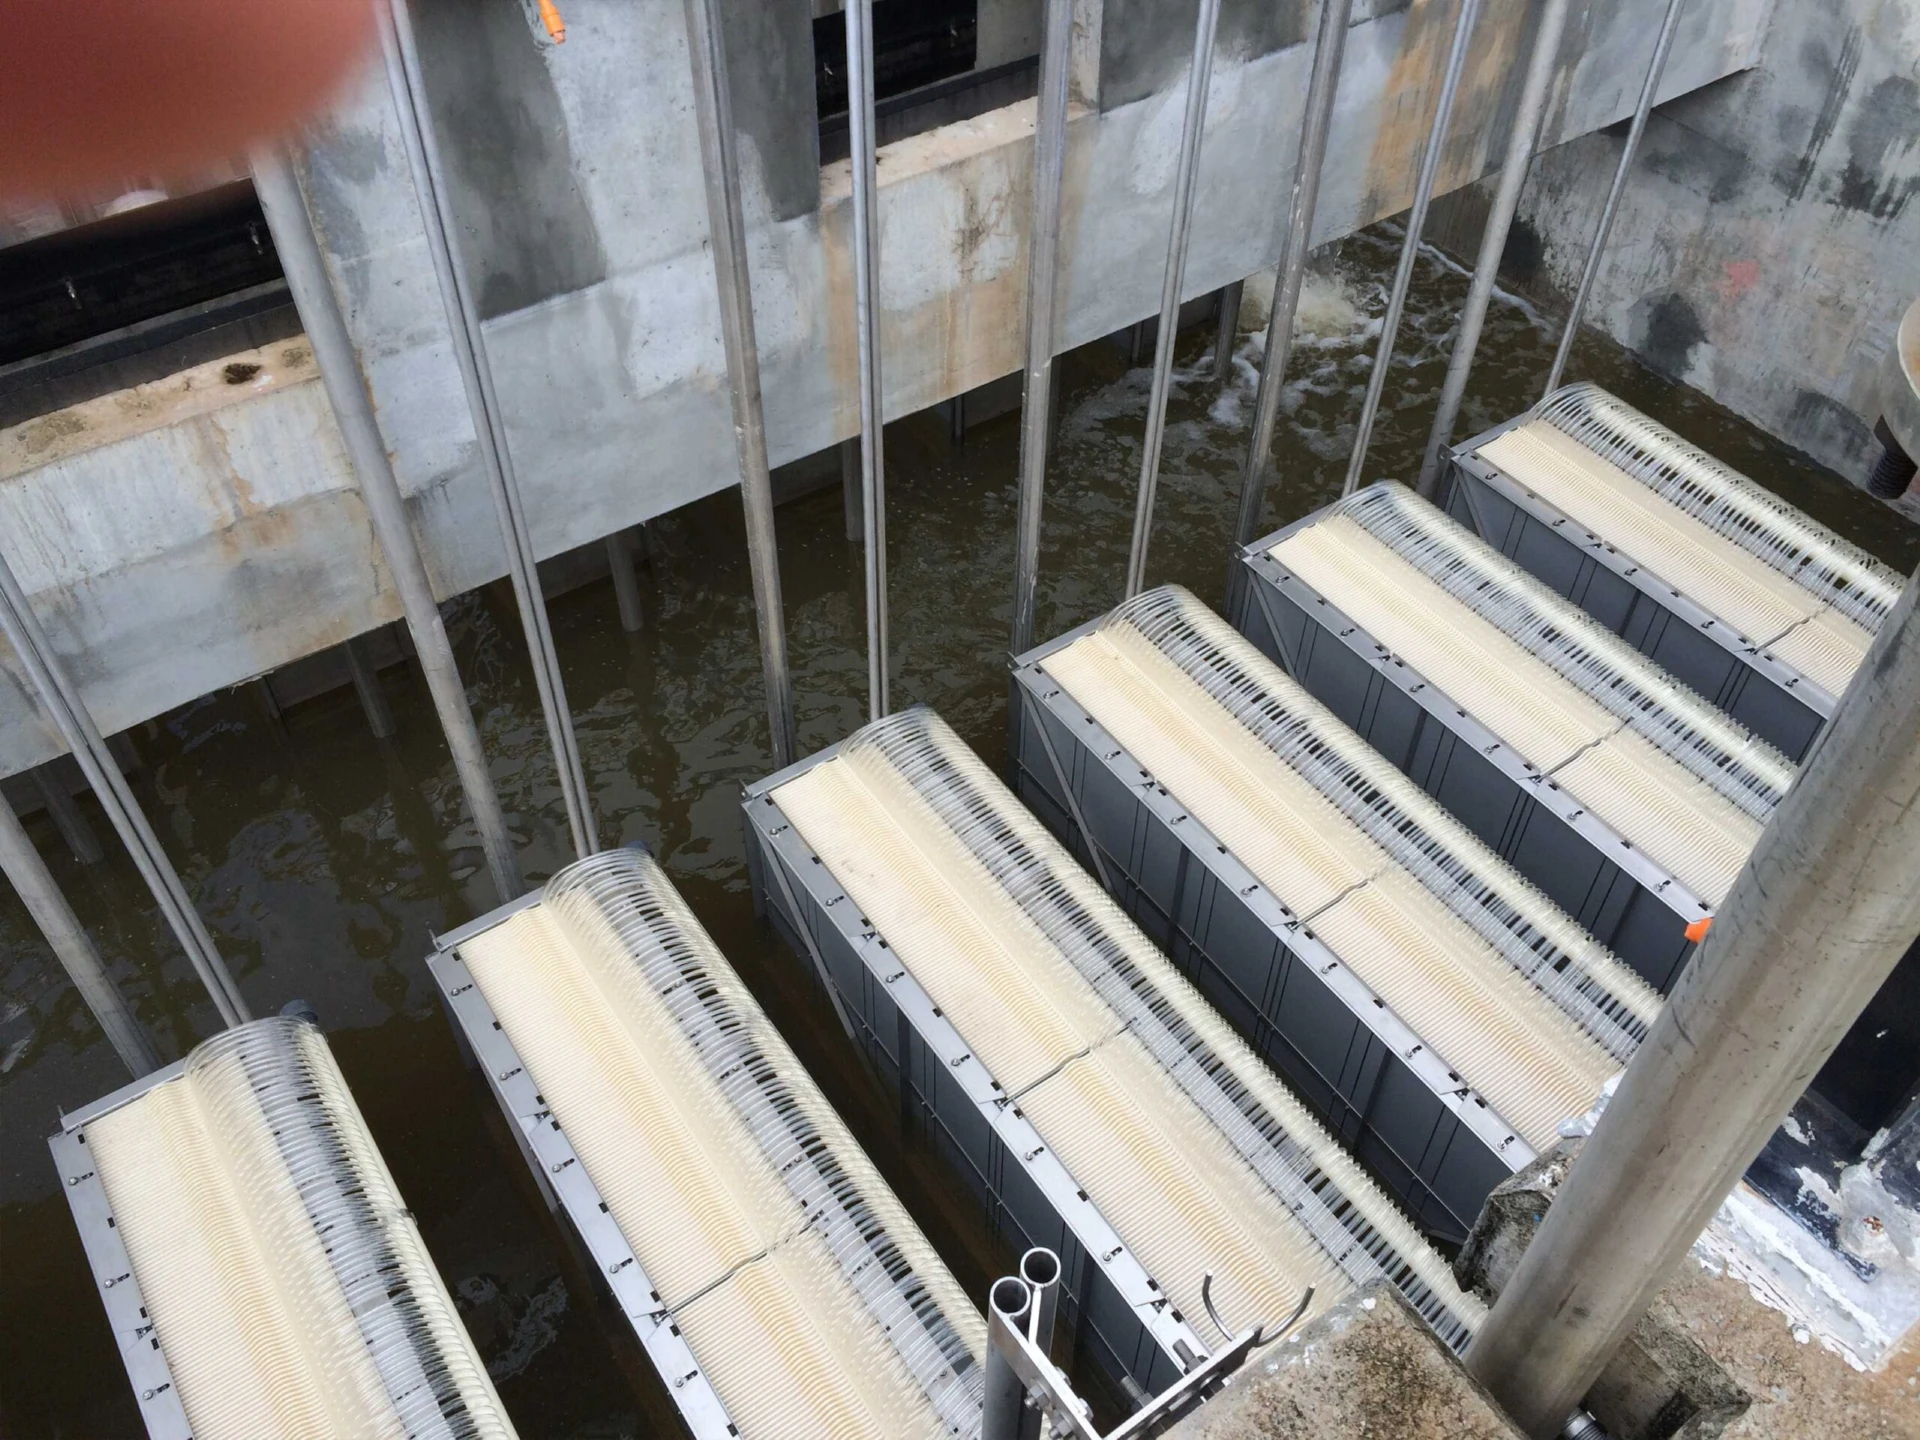
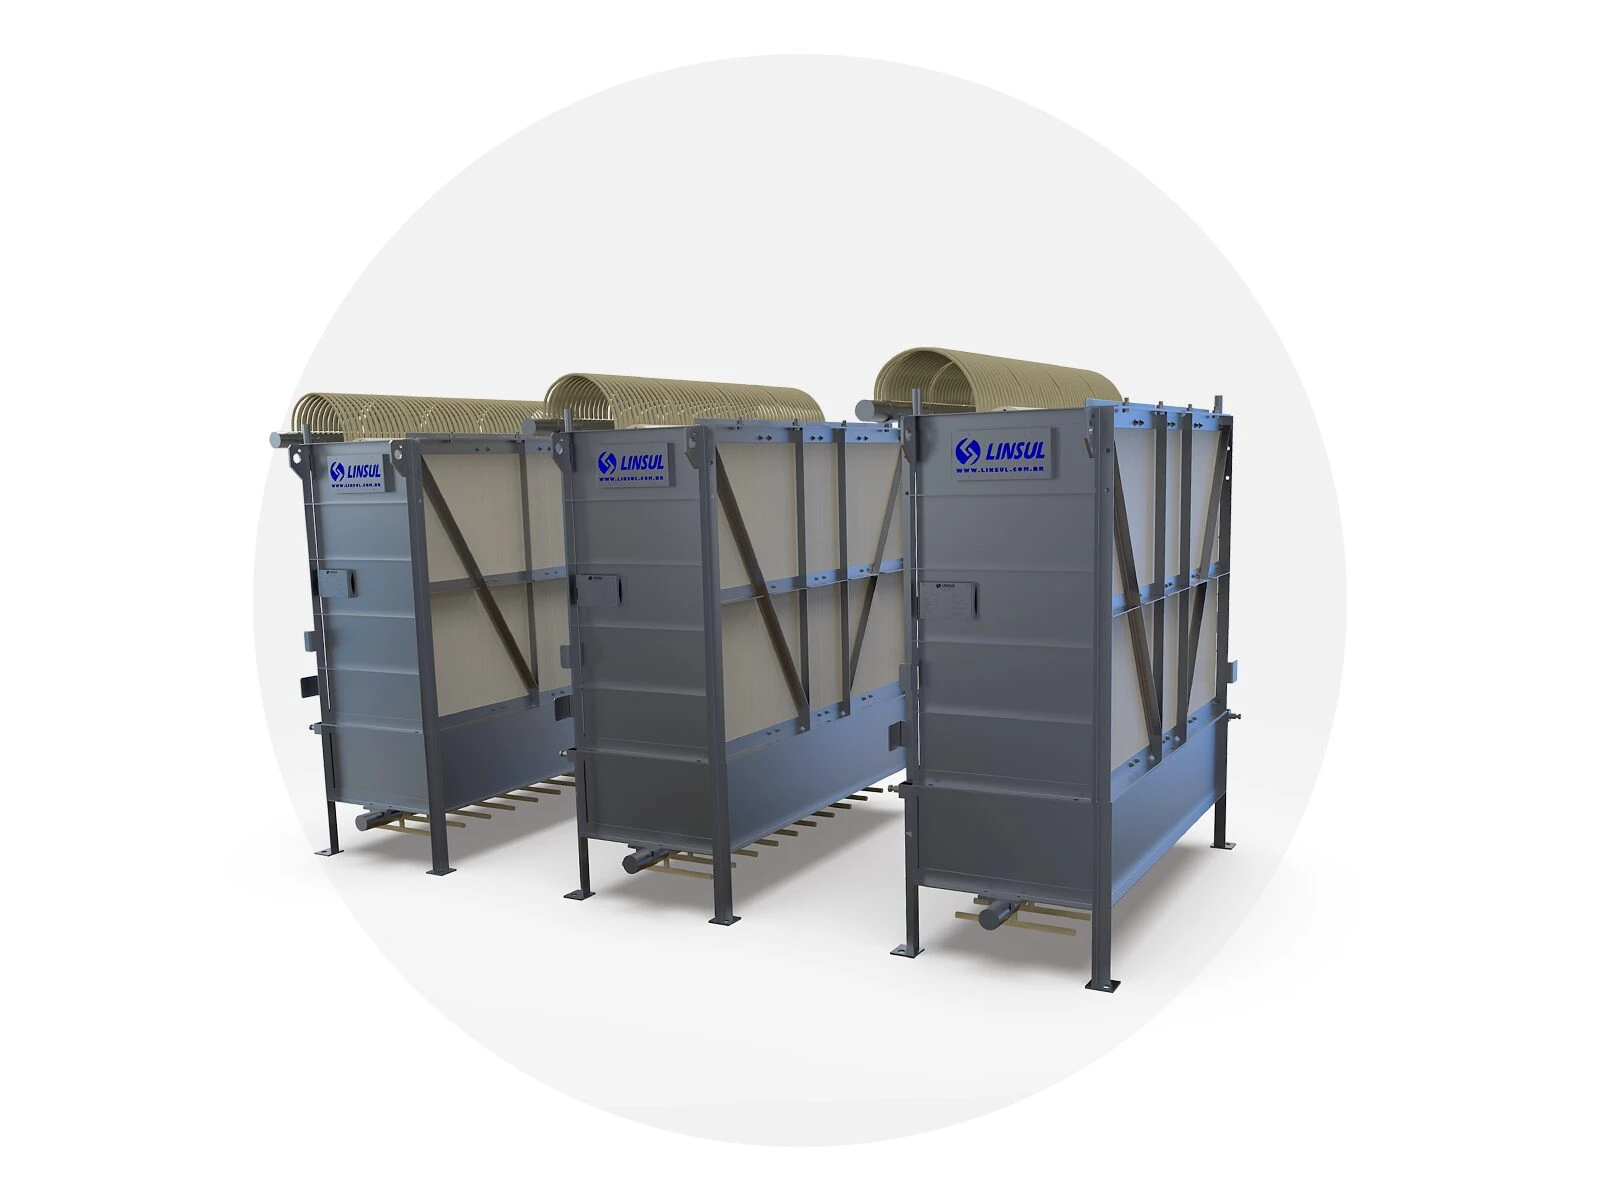
An MBR (Membrane Bioreactor) system is an advanced wastewater treatment technology that combines biological treatment processes with ultrafiltration or microfiltration membranes. This system is widely used to purify wastewater from many sources, such as domestic sewage and industrial effluents, resulting in a superior-quality treated effluent.
Features and operation
Technical details


Biological Process: Treatment begins with a biological stage, similar to a conventional biological reactor. Microorganisms, mainly bacteria, are grown in a reactor where they degrade the organic matter, nutrients and pollutants in the wastewater. These microorganisms convert organic compounds into biomass and gases.
Ultrafiltration or Microfiltration Membranes: The main feature of the MBR system is the use of ultrafiltration or microfiltration membranes to separate the biological solids from the treated effluent. These membranes are porous and act as a physical barrier, allowing the treated water to pass through while retaining solid particles, microorganisms and suspended materials.
Solid-Liquid Separation: The filtration membranes retain the biological solids and other pollutants, allowing only clean, treated water to pass through. This results in a high-quality effluent, practically free of suspended solids and microorganisms.
Sludge Return: Part of the sludge generated in the biological process is kept in the system to maintain microbial activity. However, excess sludge is removed from the MBR system, preventing excessive buildup and ensuring efficient treatment.
Space Efficiency and Compact Design: Compared to conventional systems, the MBR system takes up less physical space. This is particularly advantageous for sites with space limitations or for upgrades to existing facilities.
Flexibility and Scalability: Our MBR system is highly flexible and can be sized according to your current and future needs. This allows you to easily adapt the system's capacity to accommodate changes in wastewater load.
Resistance to Hydraulic and Load Shocks: The MBR system is designed to handle variations in wastewater load and hydraulic shocks. This ensures stable and reliable performance, even under challenging operating conditions.
Cost Reduction: Although the initial investment may be slightly higher than for conventional systems, the MBR system offers a number of long-term savings. These include lower disposal costs, space savings, less need for chemicals and greater water reuse potential.
Environmental Commitment*: By choosing the MBR system, you will demonstrate a strong commitment to environmental sustainability. The MBR system helps protect water bodies and valuable water resources.
Available capacity: 5 to 500 m³/h.
Discover the advantages of the MBR System.
We offer complete solutions for every stage of water treatment, developed to provide reliability, high performance and technical excellence in different applications.
Advantages
- Smaller footprint
- No secondary clarifiers
- Biological reactor volume up to 4 times smaller than a conventional activated sludge reactor
- Excellent treated effluent quality;
- Easy operation and maintenance
- Ability to treat difficult wastewater;
- Stable, robust process
- Low sludge production
- Easy adaptation of MBR to an activated sludge system
Applications
Treatment of wastewater with a high organic load;
Industrial wastewater treatment;
Sanitary sewage treatment;
Wastewater treatment for water reuse;
Among others.
Request a Technical analysis.
Request a technical analysis for
your operation today!
 MBR System
Why choose Linsul?
Here are some reasons:

Environmental Compliance and Legal Certainty
Our wastewater treatment systems give clients greater peace of mind, as their industries comply with strict environmental standards, avoiding fines and penalties.

Energy Efficiency and Cost Reduction
Our equipment is designed to minimize energy consumption, providing significant operational savings combined with effective, long-lasting results.
Let's talk about your project.
Count on a trained, specialized team to understand the characteristics of your operation and recommend the most suitable solution for your wastewater treatment, ensuring efficiency, safety and the best results for your process.
Talk to a specialist